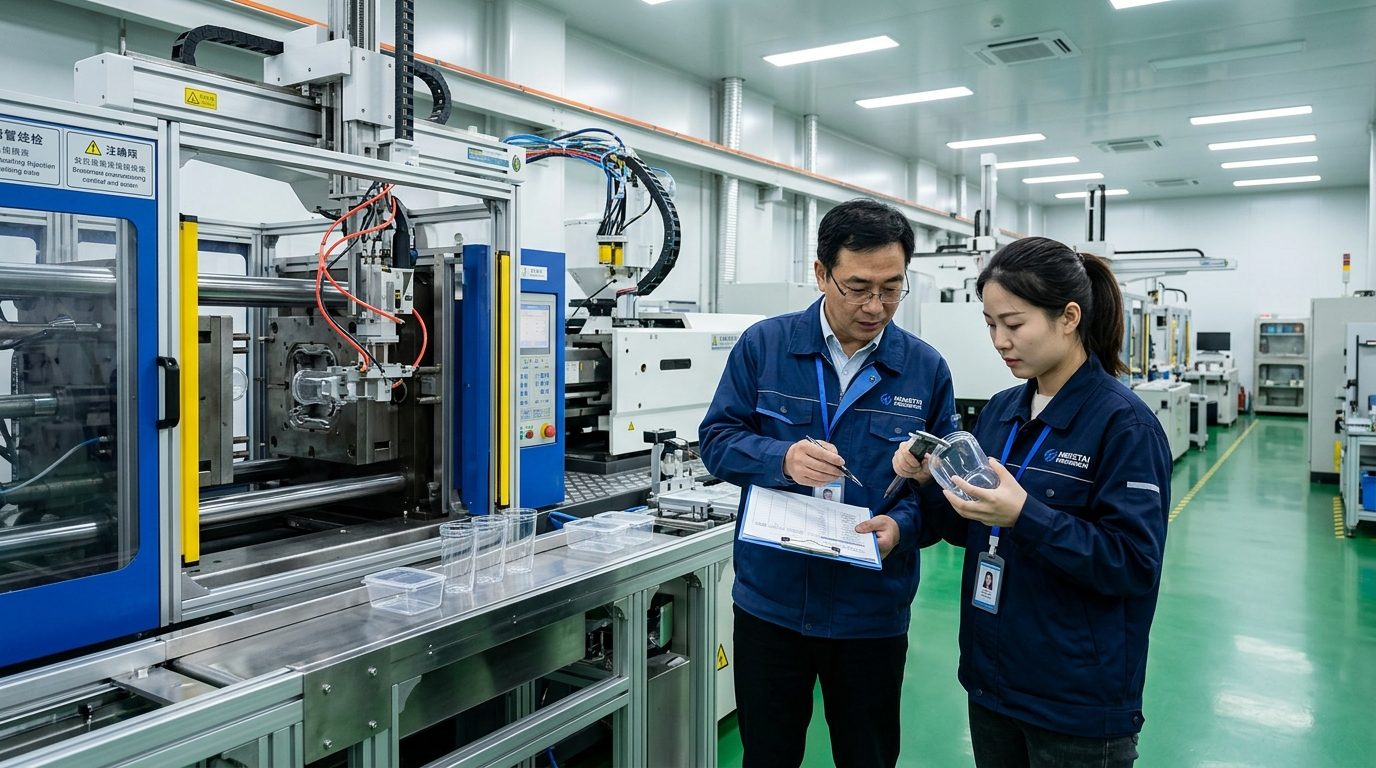
Figure 1.0: Project director and QA manager inspecting precision injection molded drinkware parts against 3D CAD tolerances on the Jinjiang cleanroom factory floor.
Launching a bespoke promotional gift program requires harmonizing industrial design, moldflow physics, and high-speed assembly. In this documented 50,000-set retail program:
- Project Scope: A 2-in-1 combo comprising a 16oz crystal-clear Eastman Tritan™ iced tumbler, a top-mounted snap-locking food-grade PP snack cup, and a custom magnetic gift box with molded pulp tray.
- Turnkey Execution Window: 35 calendar days from client 3D CAD sign-off to loaded 40ft HQ export containers at Xiamen Port.
- DFM Optimization: Adjusted bottom wall transitions from sharp 90° corners to R1.5 fillets, eliminating sink marks and reducing injection cycle time from 42s down to 31s.
- Defect Rate: Final pre-shipment third-party inspection recorded 0 critical defects, 0.4% minor cosmetic blemishes (well within AQL 2.5 Major / 4.0 Minor benchmark).
Overseas buyers often dread custom OEM development due to risks of communication lag, off-spec mold dimensions, or missed campaign launch dates. This transparent project breakdown demonstrates how our in-house engineering and production teams de-risk bespoke programs from initial napkin sketch to container dispatch.
1.0 35-Day Stage-Gate Milestone Schedule & Deliverables
Every custom OEM/ODM program is managed via structured stage-gates with signed buyer approvals before proceeding to the subsequent phase:
| Milestone Stage | Timeline Window | Engineering Tasks | Buyer Deliverables |
|---|---|---|---|
| Gate 1: DFM & 3D Feasibility | Days 1 – 3 | Parting line design, draft angle verification (1.5°), wall thickness uniformity analysis | Detailed DFM Report + 3D PDF |
| Gate 2: Functional Prototyping | Days 4 – 7 | High-resolution SLA 3D print in transparent resin + CNC POM functional threads | Physical sample kit shipped via DHL |
| Gate 3: Rapid Tooling (S136) | Days 8 – 21 | CNC high-speed roughing, vacuum heat treatment (HRC 48–52), mirror optical EDM polishing | Weekly photographic tooling report |
| Gate 4: T1 Mold Trials & Tuning | Days 22 – 25 | Trial injection, CMM dimensional measurement, seal vacuum leak testing | T1 Golden Samples + CMM report |
| Gate 5: Mass Molding & Packing | Days 26 – 33 | 50,000 units molding, automated UV silk-screen printing, retail box kitting | In-line video + AQL 2.5 Inspection |
| Gate 6: Container Loading | Days 34 – 35 | Moisture barrier palletization, container stuffing, export customs clearance | Container loading photos + Bill of Lading |
2.0 DFM & Moldflow Engineering: Eliminating Sink Marks & Weld Lines
During initial design evaluation of the client's dual-compartment concept, our moldflow simulation software identified two severe failure risks:
DFM Problem & Solution Matrix
- Risk: Heavy Sink Marks at the Tumbler Base. The original CAD draft specified a 4.2mm thick solid bottom plate transitioning into 1.8mm sidewalls. This differential would cause severe shrinkage sink marks. Engineering Solution: We cored out the base with a stepped rib lattice, equalizing nominal wall thickness to 2.0mm ± 0.1mm, speeding up mold cooling by 26%.
- Risk: Cosmetic Weld Line Across Straw Hole. Plastic flow fronts meeting at the straw orifice would create a visible knit line prone to stress cracking. Engineering Solution: Relocated the direct sub-gate from the top rim to the underside flange, moving weld lines to an invisible non-stressed region.
- Draft Angle Optimization: Increased core draft angle from 0.5° to 1.5° to guarantee scuff-free ejection on high-gloss Eastman Tritan™ surfaces.
3.0 Prototyping Validation: SLA 3D Print vs CNC Machined First Article
Prior to cutting steel, physical prototypes verify ergonomic grip, volumetric fluid capacity, and lid snap-fit feel:
- SLA 3D Printing (Photosensitive Acrylic): Within 48 hours, we 3D printed full-scale assemblies. This confirmed the 16oz fluid capacity and validated the hand-feel for both adult and juvenile consumers.
- CNC Machined Polyoxymethylene (POM / Acetal): While 3D prints evaluate aesthetics, threaded closures require precise CNC machining. We machined matching screw threads in POM to test thread engagement torque and drop impact resistance.
- Client Sign-Off: The prototype kit was dispatched via DHL Express, arriving at the client's Chicago headquarters in 3 business days for retail merchandising sign-off.
4.0 Rapid Tooling Fabrication (S136 Steel) & T1 Trial Tuning
With signed CAD approval, our in-house Jinjiang tooling shop initiated CNC mold fabrication:
| Component Mold | Steel Specification | Cavity Layout | Hot Runner System | Cycle Time |
|---|---|---|---|---|
| 16oz Tumbler Body | Grade S136 (HRC 48–52 Mirror) | 2-Cavity Balanced | Yudo Valve-Gate Hot Runner | 31 Seconds |
| Snack Top Cup | Grade NAK80 (Pre-hardened) | 4-Cavity Balanced | Direct Hot Sprue | 22 Seconds |
| Silicone Sealing Ring | Cr12MoV Tool Steel | 16-Cavity Compression | Heated Compression Platen | 180 Seconds |
5.0 Mass Molding, Silk-Screen Decoration & In-Line AQL 2.5 QA
Mass production was executed across two synchronized 320-ton Haitian precision servo injection presses:
- Robotic De-Molding: High-speed 3-axis servo robots retrieved parts from open mold cavities, placing them directly onto clean dust-free conveyer belts to eliminate cosmetic fingernail scratches.
- Automated UV Silk-Screen Printing: 2-color high-definition logos applied using automated rotary UV screen-printing lines. Ink adhesion passed ASTM D3359 cross-hatch tape testing (Grade 5B, 0% flaking) after 50 continuous dishwasher cycles.
- Pre-Shipment Inspection (PSI): Final AQL 2.5 Major / 4.0 Minor inspection audited 500 sampled units: zero liquid leakage at 35 kPa vacuum differential, zero structural cracking after 1.5m drops onto concrete.
Planning a Custom Drinkware or Container Project?
Speak directly with our tooling engineers. We provide comprehensive DFM evaluations, 3D CAD modeling, and transparent open-book tooling quotes within 24 hours.
Turnkey OEM/ODM Development FAQ
Who owns the intellectual property and injection molds once built?
The client retains 100% full legal ownership of all custom injection molds, CAD designs, and project tooling. We sign binding Mutual Non-Disclosure Agreements (NDAs) and never share or reuse custom tooling for any third-party client.
Can you handle retail packaging assembly and Amazon FBA pallet prep?
Yes. Our Jinjiang facility houses integrated dust-free assembly cleanrooms. We assemble the drinkware components, insert silicone gaskets, package into custom retail gift boxes, apply retail barcode stickers, pack into master export shippers, and stretch-wrap pallets to your exact warehouse specifications.
What is your warranty policy if any defect occurs during shipping?
We stand behind our manufacturing with a 100% replacement or credit guarantee for any defect exceeding our agreed AQL 2.5 threshold. Every production lot retains golden archive samples and serialized quality inspection logs for full traceability.
Turnkey OEM Project Misconceptions Debunked
❌ Myth 1: "Sourcing Components from Multiple Sub-Vendors is Cheaper Than Turnkey OEM"
✔ Engineering Reality: Multi-vendor sourcing creates 'interface gaps': the silicone sleeve doesn't fit the glass tumbler, or the gift box is 3mm too small for the lid. Turnkey manufacturing at Naike Gifts guarantees single-point CAD ownership, synchronized Pantone color matching, and unified quality accountability.
❌ Myth 2: "Custom Multi-Piece Gift Sets Require Minimum 10,000 Unit Commitments"
✔ Engineering Reality: Through modular tooling inserts and digital packaging proofing, our factory enables pilot production runs starting at 1,000 to 2,000 sets, allowing cross-border brands to validate marketplace traction before capital-intensive mass orders.
❌ Myth 3: "E-Commerce Fulfillment Packaging Can Use Standard Retail Rigid Boxes"
✔ Engineering Reality: Rigid retail boxes crush easily in warehouse sortation conveyors. E-commerce gift sets require double-corrugated (E/B-flute 450gsm) outer master shippers with edge crush test (ECT > 44 lbs/in) ratings.